Single Bucket Elevator Manufacturer for Vertical Material Feeding
Jiaxing K-Line Machinery Co., Ltd. supplies the Single Bucket Elevator Manufacturer range for automated packaging lines. We build vertical lifting equipment that moves granules, pellets, powders and other free-flowing products from floor level into hoppers, weighers or packing machines. The single bucket elevator is a straightforward and easily maintained solution, and we customize each unit to the required height, capacity, discharge point and control interface.
Our machines are designed and manufactured under the supervision of a senior technical team with nearly two decades of automated packaging experience. From our factory in Jiaxing, China, we support food, agricultural, chemical and hardware industries with reliable material conveying and complete line integration.
Where a Single Bucket Elevator Fits in Your Line
A single bucket elevator is selected when the line needs a controlled vertical lift without the complexity of continuous conveying. It is typically placed between a bag dump station or storage hopper and a weighing or packaging machine. Once the bucket reaches the upper level, it discharges into a Vertical Packaging Machine or into a multi-head weigher that feeds the packer.
- Feeding from bag dump, tipping station or silo outlet
- Lifting to a multi-head weigher, linear weigher or volumetric filler
- Raising product between floor levels or across line elevations
- Batch feeding where product must be released on demand
Material and Product Considerations
Because a bucket elevator lifts discrete volumes, it suits products that flow freely and do not pack or bridge easily. Typical materials include nuts, beans, seeds, candies, dried fruit, granules, and some powders. We confirm bulk density, particle size and flow characteristics before configuring bucket geometry, lifting speed and discharge angle.
Critical Specifications We Define with You
- Lift height and overall machine height
- Bucket volume, fill rate and target throughput
- Motor power and reducer ratio
- Infeed hopper size and discharge spout orientation
- Control voltage and interface to existing equipment
Configuration Options
Customization is central to our single bucket elevator offering. We adjust the mechanical design, control logic and material contact surfaces so the machine matches the product and the production line.
- Bucket and contact materials for food or aggressive products
- Lift height, discharge height and support structure
- Infeed hopper volume and discharge spout orientation
- Free-standing or line-mounted design
- OEM configurations based on customer drawings or line layout
- Motor, reducer and speed selection matched to throughput
Related Conveying Equipment Range
Single bucket elevators are one of the five conveying families in our Material Feeding and Conveying Equipment range. For continuous feeding at higher rates, our Z-type Elevator provides vertical transport with horizontal inlet and outlet sections. The table below shows how we position each machine type.
| Machine |
Typical Function |
Best-Fit Products |
| Single Bucket Elevator |
Vertical lift in discrete batches with simple structure and easy maintenance |
Nuts, beans, candies, granules, dried fruit |
| Z-type Elevator |
Continuous vertical transport with horizontal inlet and outlet |
Snacks, pellets and granules feeding weighers |
| Inclined Conveyor |
Incline transfer from bag dump or hopper |
Fragile, irregular or bulky products |
| Screw Elevator |
Enclosed dust-tight vertical conveying |
Powders and fine granules |
| Vacuum Loader |
Pneumatic transfer from bags, drums or silos |
Powders and granules requiring dust-free loading |
Controls, Automation Integration and Safety
Material feeding and conveying equipment in our range is supplied with control circuits and level sensors for automatic feeding and stopping. When the weigher or packaging machine consumes product, the elevator starts and stops according to the level signal, which avoids manual attention and keeps the line balanced.
We coordinate the elevator control logic with existing line PLCs or relays. For a complete automated line, we also design the inlet and outlet transitions, support framing and operator access. Standard safety provisions include guarding, emergency stop, and clear warning labels.
Quality Assurance and Project Support
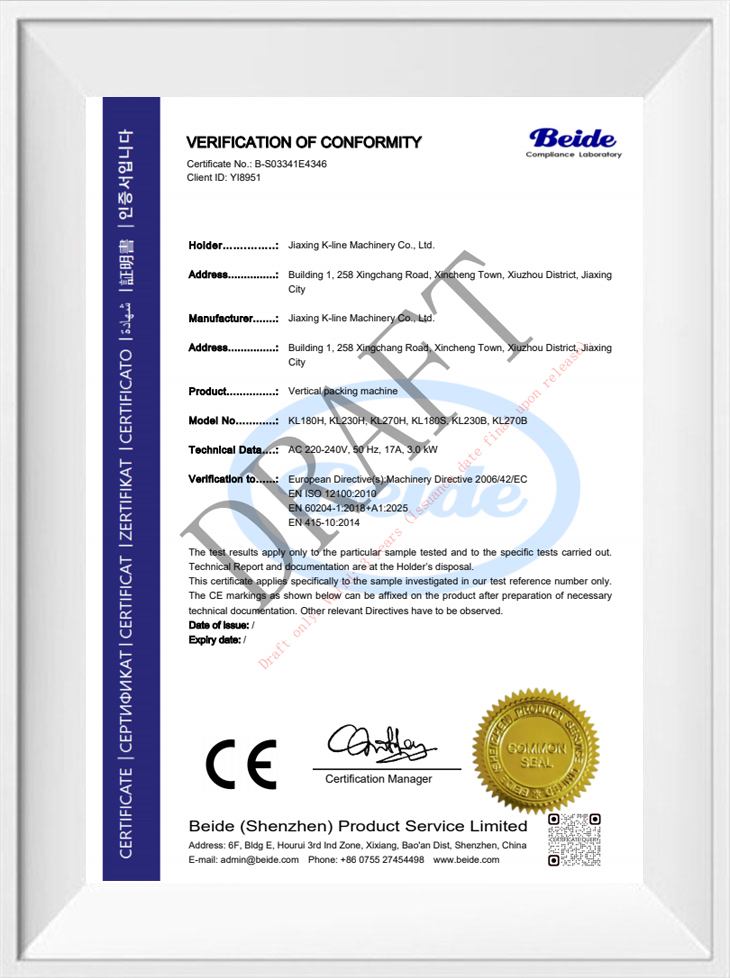
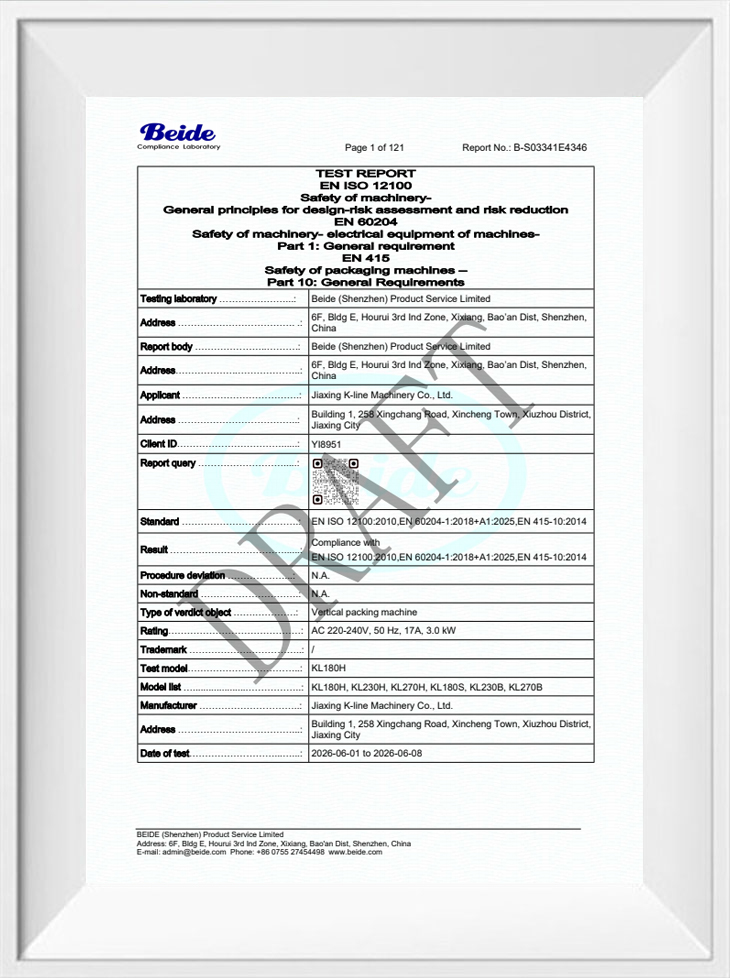
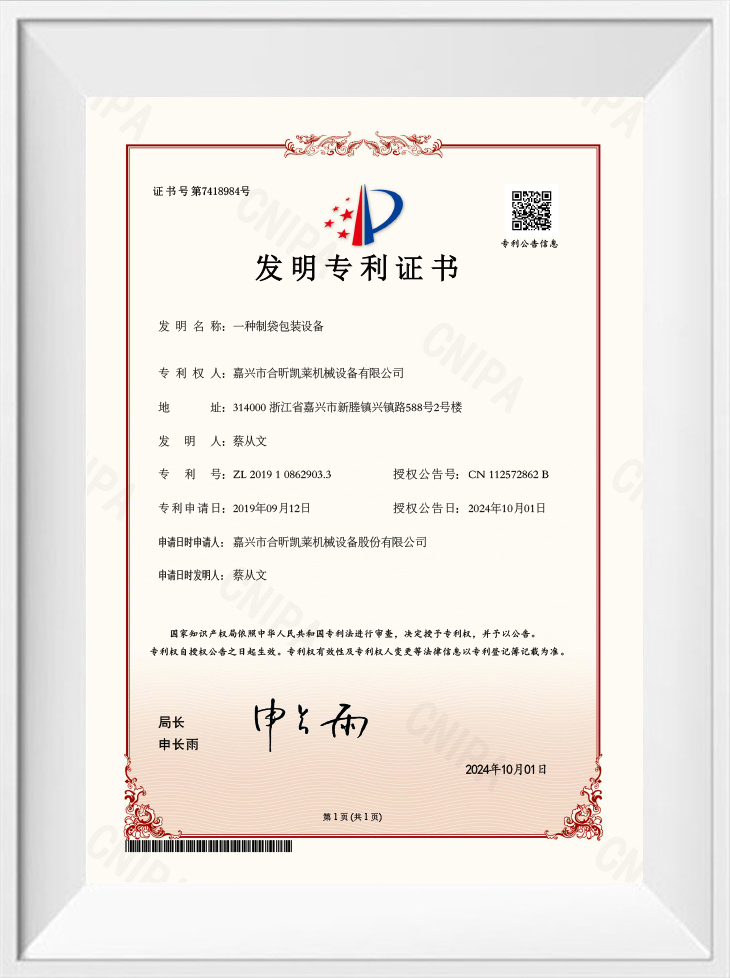
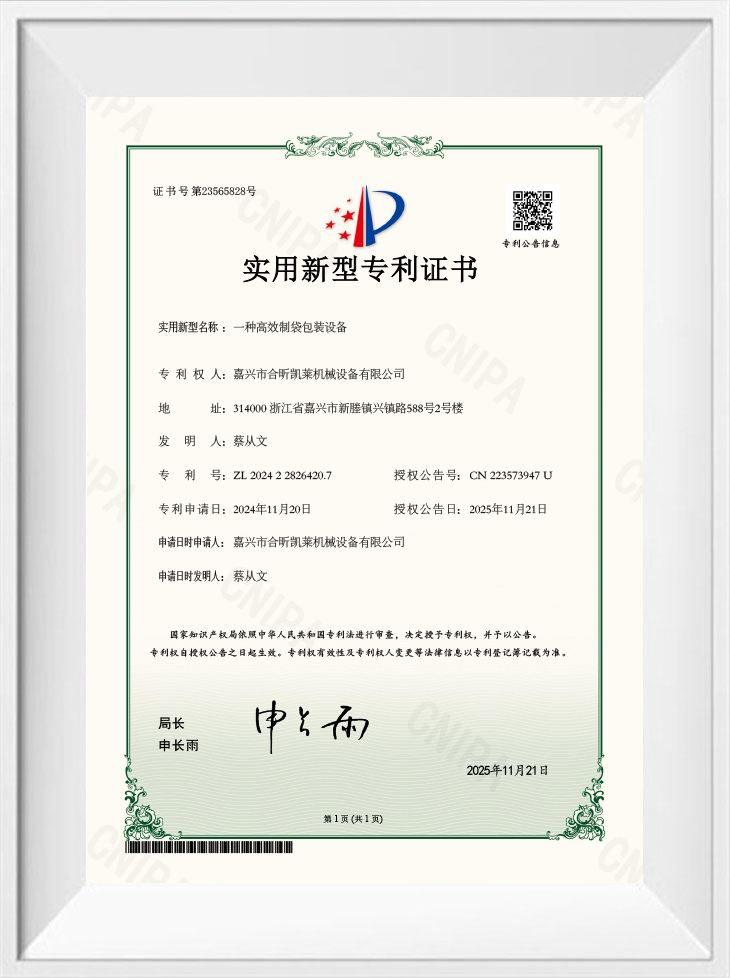
R&D, design and manufacturing are supervised by senior technical staff, and our certification records include CE test draft reports plus multiple invention and utility model patents for packaging and conveying machinery. The same technical team that designs the line supports commissioning and after-sales service.
Our project support covers detailed drawings, installation guidance, commissioning assistance, spare parts and remote troubleshooting. For full-plant projects, we undertake integrated design and turnkey implementation of automated packaging systems.
Information We Use to Configure Your Solution
When you request a proposal, we prepare the configuration around the actual product and line conditions. The following points help us size the bucket, hopper, motor, support structure and control interface.
- Product type, bulk density, particle size, flowability, moisture and temperature
- Required lift height and distance from infeed to discharge
- Target throughput in kg/hr or bags/min
- Infeed source and discharge destination (weigher, hopper or packing machine)
- Available floor space, ceiling height and access for maintenance
- Electrical supply: voltage, phase and frequency
- Product contact material requirements, including food-grade or washdown surfaces
- Existing control interface, line PLC or interlock requirements
Frequently Asked Questions
Can a single bucket elevator handle fragile products?
Yes, with appropriately selected bucket size, lifting speed and discharge angle. We slow the lifting speed and adjust the outlet geometry so fragile items are not damaged during transfer.
What is the difference between a single bucket elevator and a Z-type elevator?
A single bucket elevator lifts in discrete batches and is normally used for simpler vertical transfer. A Z-type elevator provides continuous vertical transport with integrated horizontal inlet and outlet sections, which is better for high-throughput weigher feeding.
How do you integrate the elevator with our existing line?
Provide the discharge height, destination machine, control voltage and existing PLC signals. We supply the elevator with matched inlet and outlet transitions and level sensor logic so it starts and stops automatically with the line.
What material options are available for food-contact parts?
We select food-grade stainless steel or food-grade polymer based on the product, abrasiveness and cleaning requirement. For washdown environments, stainless steel contact parts and sealed bearings are used.
Do you support installation and commissioning?
Yes. We provide detailed drawings, installation guidance and commissioning assistance, and our after-sales team supports remote troubleshooting and spare parts for the complete elevator.
 English
 中文简体
 Español
 русский