Packaging Line Automation Equipment Factory

Home / Product / System Equipment

Packaging Line Conveying System Manufacturer

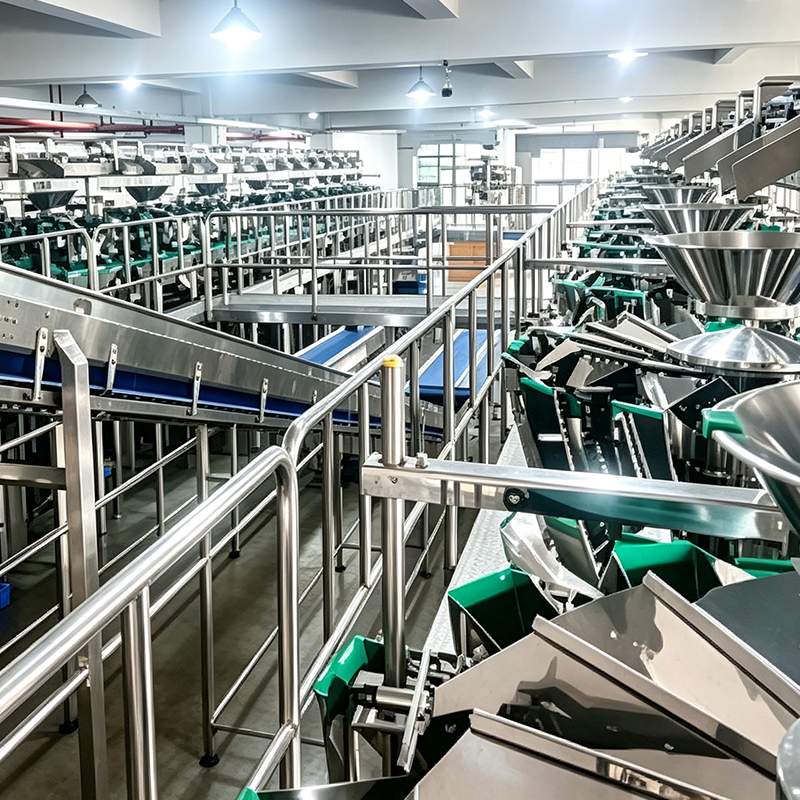
System equipment includes fast return conveyors, sorting conveyor belts, multi-outlet bucket elevators, multi-outlet screw conveyors, feeding cart conveyors, integrated conveyor platforms, and case packing robots, featuring 304 stainless steel main structures and food-grade materials, with waterproof design, variable frequency speed control, and intelligent control functions. As system-level solutions for packaging production lines, these machines achieve full-process automation of material distribution, conveying, integration, and palletizing, improving overall production efficiency and intelligence.

About
Jiaxing K-Line Machinery Co., Ltd.
Jiaxing K-Line Machinery Co., Ltd. is a comprehensive service provider of automated packaging machinery, focusing on the mid-to-high-end domestic and overseas markets.
Our core team has been engaged in the automated packaging industry for nearly two decades. The entire process of product R&D, design, and manufacturing is strictly supervised by senior technical staff. Drawing on well-established technologies, we deliver high-performance and highly reliable automated packaging systems.
Located in Xiuzhou District, Jiaxing City, the company sits on the economically prosperous and conveniently accessible Hangzhou-Jiaxing-Huzhou Plain, adjacent to major Yangtze River Delta cities including Shanghai, Hangzhou, Ningbo, and Suzhou.
Leveraging the region's advantages in talent, information, and precision processing, we specialize in the R&D, production, and sales of vertical automatic weighing packaging machines and supporting conveying systems.
We are a China Packaging Line Conveying System Manufacturer and Packaging Line Automation Equipment Factory, offer a complete product portfolio, covering vertical automatic packaging machines, automatic premade pouch packing machines, conveying equipment, customized non-standard machinery, branded weighing equipment, back-end packing & sorting equipment, and on-line checking equipment. We are capable of undertaking integrated design and turnkey implementation of full-plant automated packaging systems. Our products are widely applied in multiple industries such as confectionery, puffed food, biscuits, powder materials, nuts, frozen food, agricultural and sideline products, chemical materials, and hardware products.
The company has built an all-round marketing network supported by a standardized full-cycle after-sales service system, providing one-stop full-process service guarantees for global customers. We take international quality, Taiwan technology, and mainland pricing as our market foothold, and pursue win-win development together with employees and partners.
Certificates of Honor
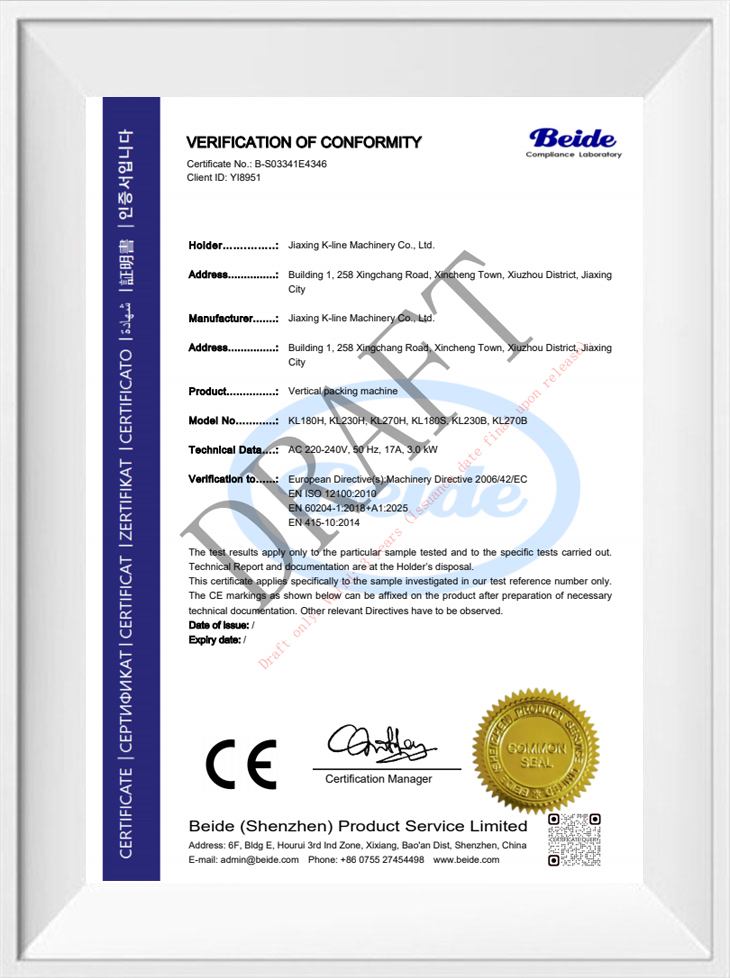
  • CE
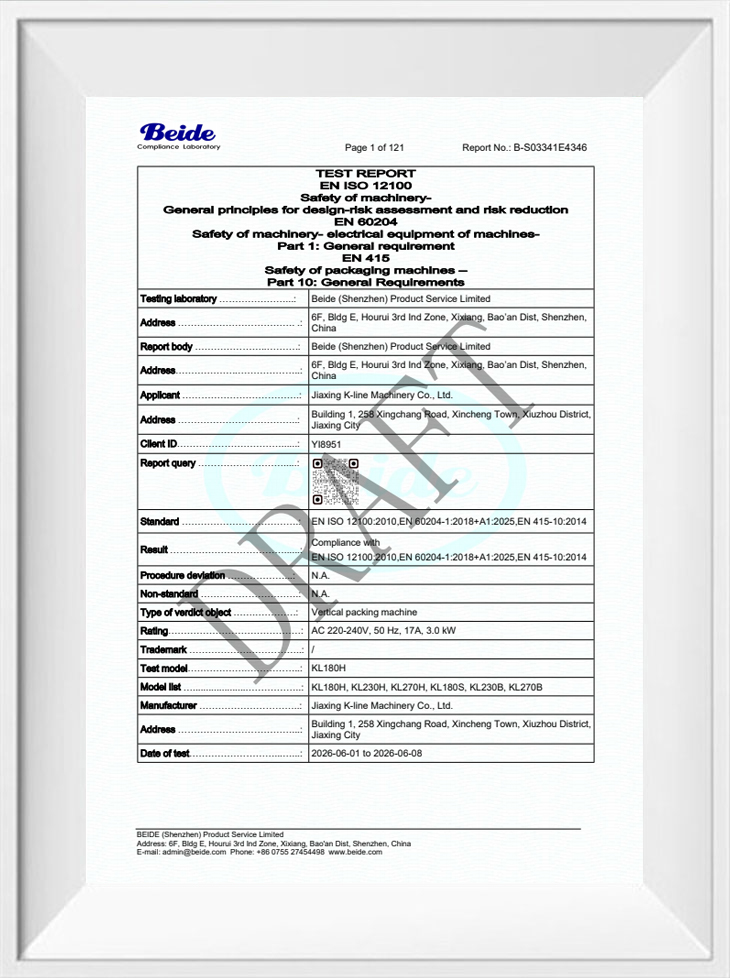
  • Test  Draft Report
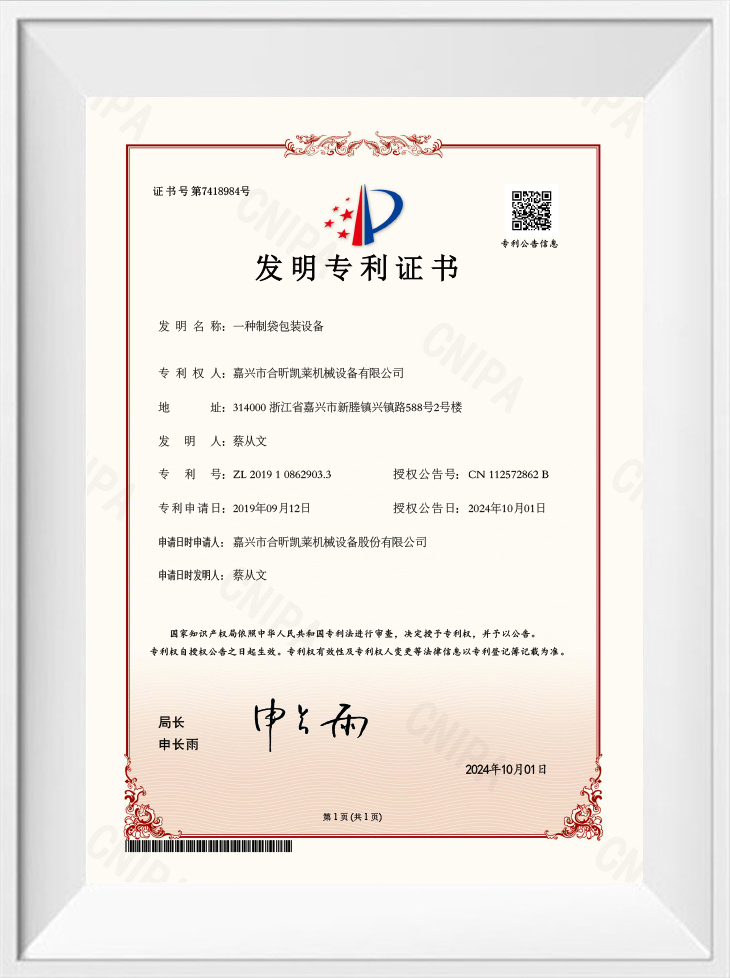
  • Invention Patent
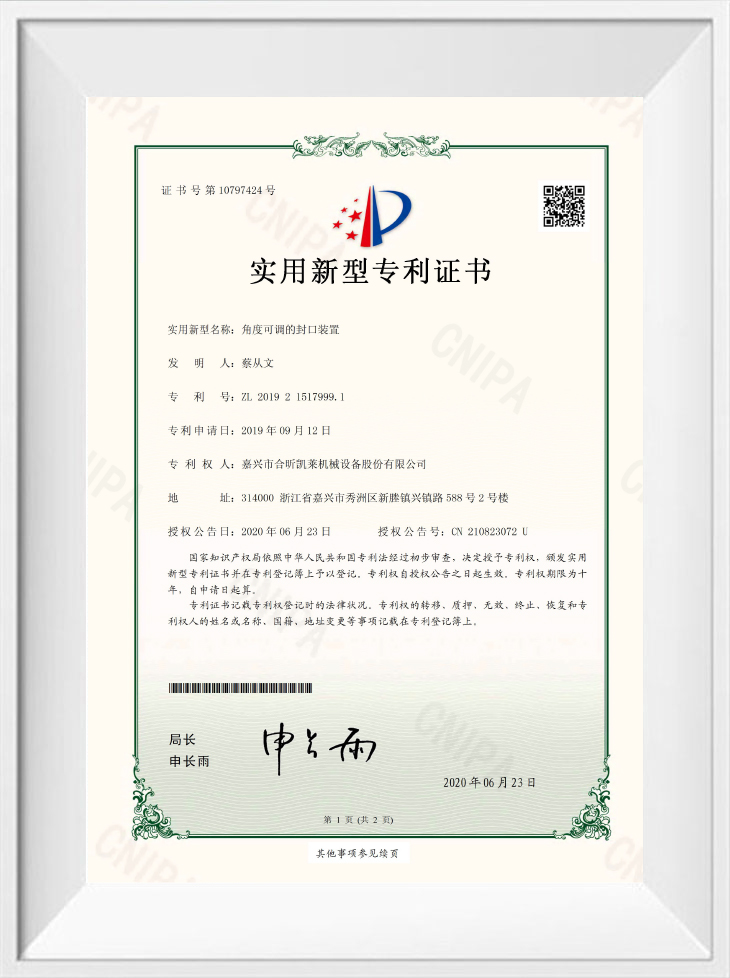
  • Utility Model Patent
  • Utility Model Patent
  • Utility Model Patent
  • Utility Model Patent
  • Utility Model Patent
  • Utility Model Patent
  • Utility Model Patent
  • Utility Model Patent
  • Utility Model Patent
News
System Equipment Industry knowledge

System Equipment: the integration layer of an automatic packaging line

At Jiaxing K-Line Machinery Co., Ltd., System Equipment is the conveyor and automation layer that connects weighing, filling, inspection, case packing and palletizing. We are a Packaging Line Conveying System Manufacturer, supplying fastback conveyors, material distribution conveyors, multi-outlet bucket elevators, multi-outlet screw conveyors, feeding cart conveyors, integrated conveyor platforms, case packing robots and palletizing robots. The range is built around 304 stainless steel main structures and food-grade contact materials, with waterproof design, variable frequency speed control and intelligent control functions.

These machines are used for confectionery, puffed snacks, biscuits, powders, nuts, frozen food, agricultural and sideline products, pet food, chemical materials and hardware. Together with our Packaging Equipment and Vertical Packaging Machine ranges, we are able to deliver complete automatic packaging line equipment from a single source.

The System Equipment range we manufacture

Each unit in the range has a defined role: feeding, dividing, lifting, distributing or end-of-line handling. The table below is the starting point for a configured solution.

Equipment Function in the line Typical line position
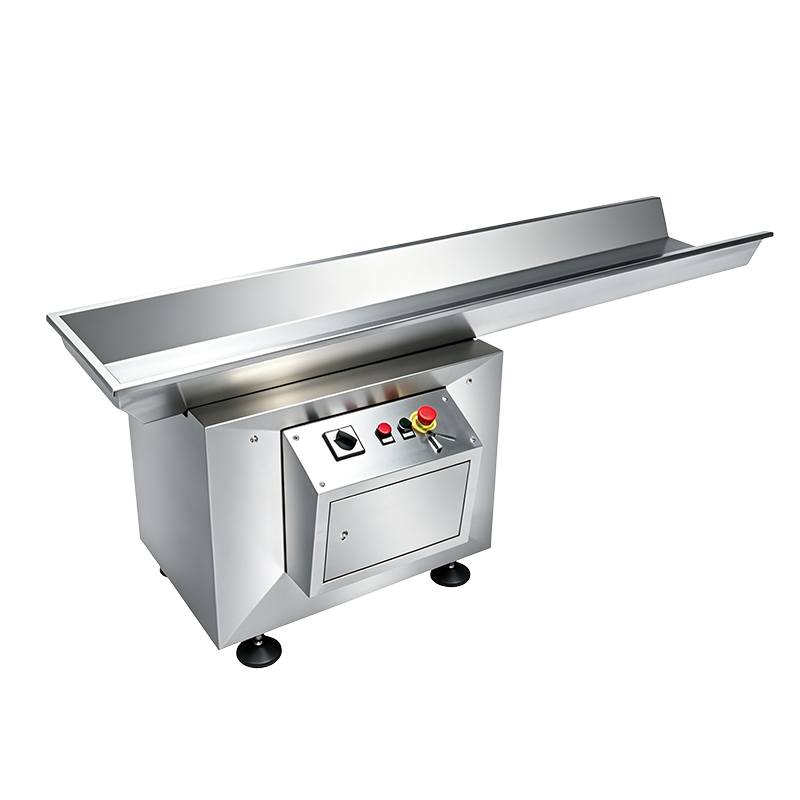
Fastback Conveyor Horizontal motion moves fragile, layered or seasoning-coated product without drop damage; stainless tray removes for cleaning. Feeds multi-head weighers before bagging.
Material Distribution Conveyor Belt sections and rotary blocking mechanisms divert product to one of several destinations. Between a single supply source and multiple packaging machines or inspection units.
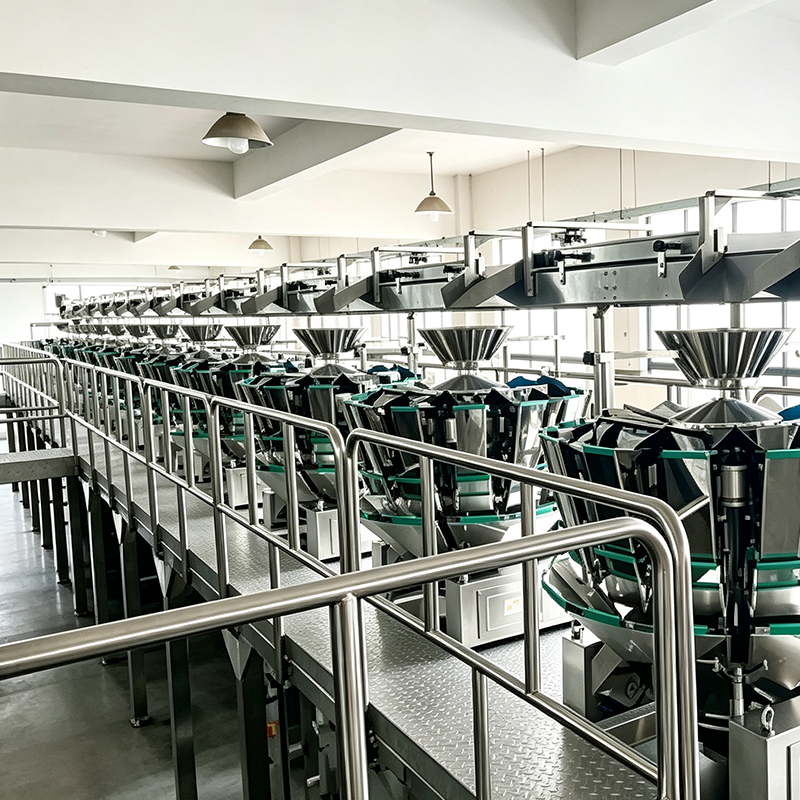
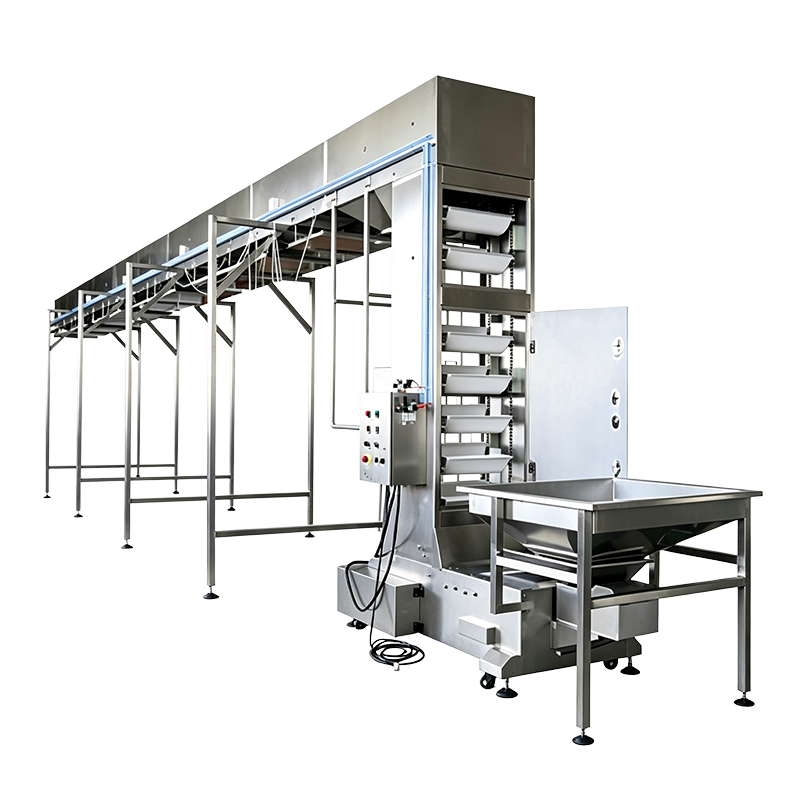
Multi-Outlet Bucket Elevator Vertical bucket lift with multiple discharge points distributes granular material at a controlled rate. Upstream of multi-head weighers or packaging machines.
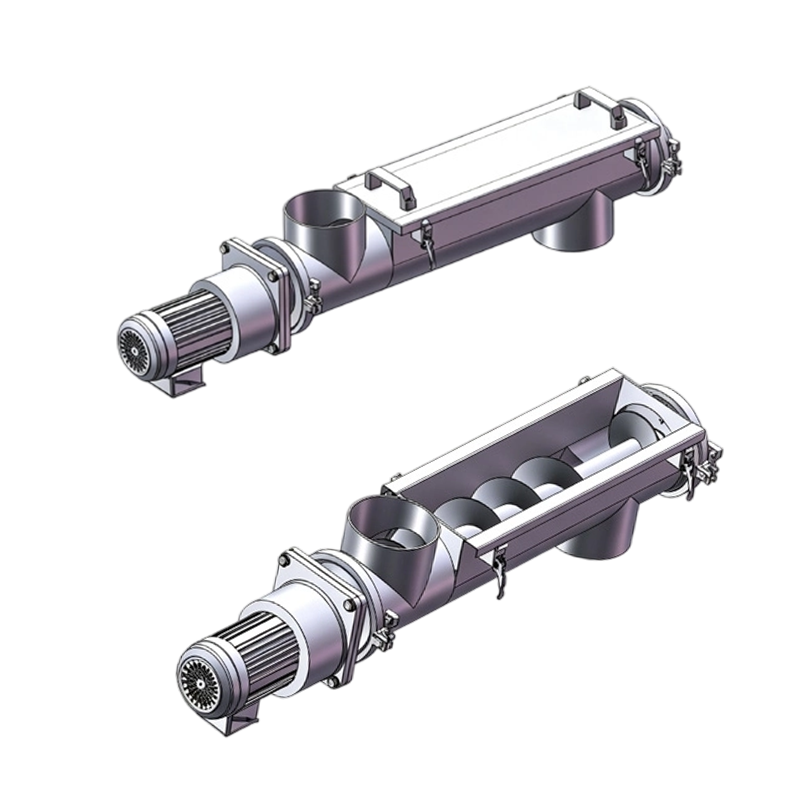
Multi-Outlet Screw Conveyor Sealed U-shape horizontal screw transfers and divides powder or granules to several filling stations. Between hoppers, silos and bagging lines.
Feeding Cart Conveyor Buffered transfer of bags or packs keeps end-of-line flow stable. Before case packing or palletizing.
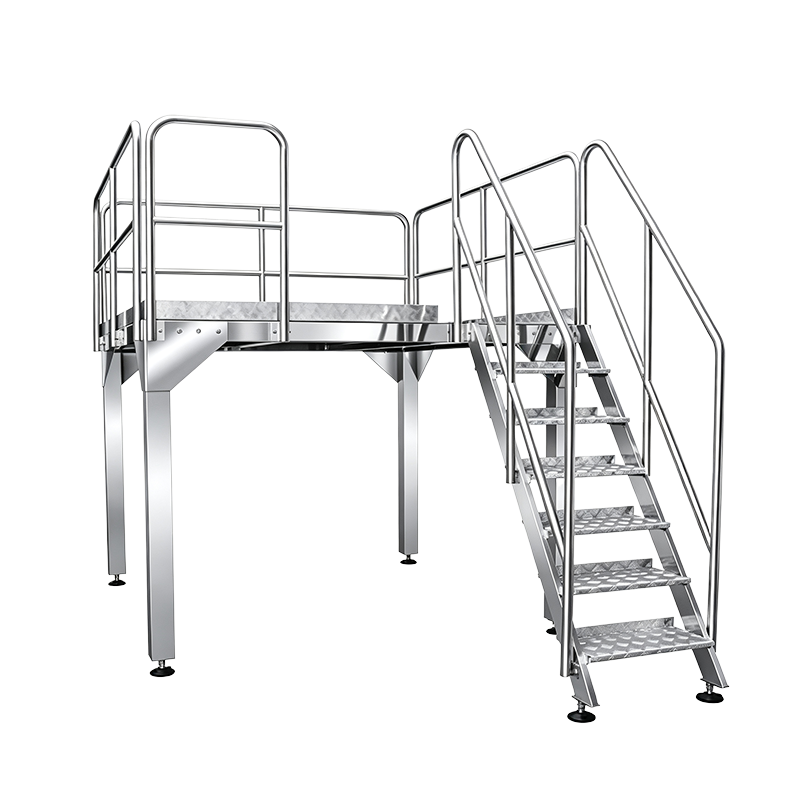
Integrated Conveyor Platform Multi-connected conveyor and working platform layouts support several machines on one compact structure. Around multi-line packaging and inspection systems.
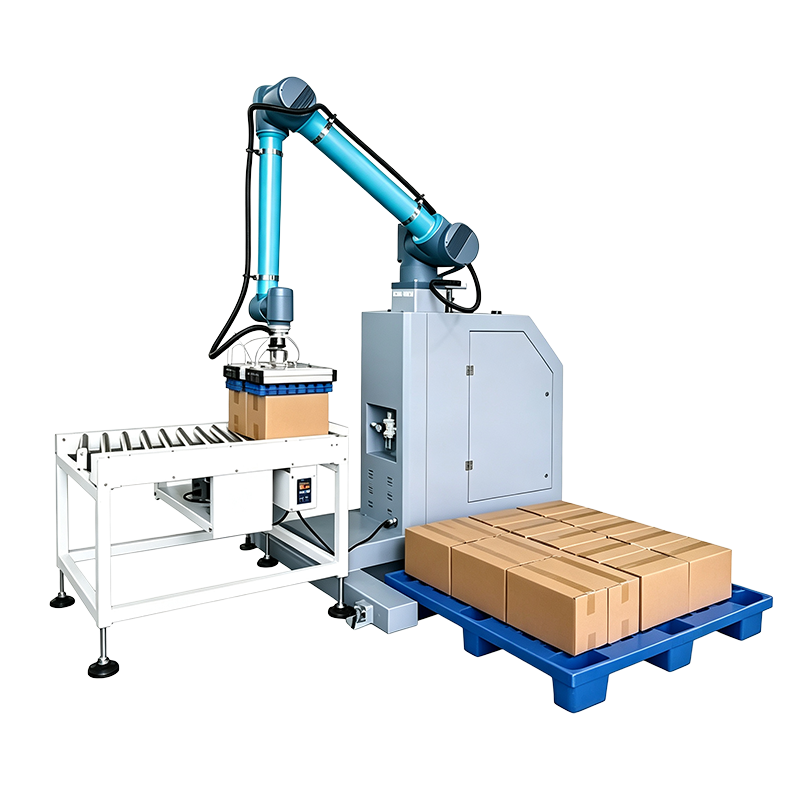
Case Packing Robot Automatic case packing for bags and pouches at the end of the packing section. After product inspection, before case sealing.
Palletizing Robot Collaborative palletizing workstation stacks cases or bags onto pallets. Final position on the line.

Material handling and process fit

Fragile and coated products

Fastback Conveyors use horizontal motion rather than vibration or drops to move product to a multi-head weigher. Standard tray length is 2000 mm, with 1800-3500 mm available; tray width is 410 mm and tray height is 100 mm. Power is 1.5 kW and the unit is rated IP54. The fully stainless steel structure and removable tray make the conveyor suitable for potato chips, frozen foods and candies with seasoning or coating that must not be knocked off.

Granular materials and multi-outlet distribution

For rice, tea, feed, chips, peanuts, candy, dried fruit, vegetables, frozen product and chemicals, Multi-Outlet Bucket Elevators provide vertical lifting with capacities of 2-12 m3/h. Bucket volume options are 1-6.5 L; the standard 1.8 L unit has a height of 3896 mm and a discharge height of 3256 mm, with 0.75 kW power. Food-grade PP/ABS buckets and 304 stainless or carbon steel frames allow the elevator to feed weighing and packaging machines directly.

Multi-Outlet Screw Conveyors add sealed U-shape horizontal transfer for powders and granules. This configuration suits applications where product must be divided to several filling stations without dust escape.

Multi-line layout and end-of-line integration

Material Distribution Conveyors operate at 1-30 m/min with food-grade PU belts and SUS304 outer frames. Rotary blocking mechanisms on the belt direct product to one of several destinations, which makes it practical to pair one supply line with multiple packaging machines or inspection devices. Integrated conveyor platforms and feeding cart conveyors create the compact buffer zones needed before case packing and palletizing. Case packing robots and collaborative palletizing workstations complete the line.

Automation integration and control

Variable frequency speed control is used across the range to match conveyor speed to the production rate. Intelligent control functions coordinate material flow so a single upstream source can feed multiple weighers or baggers without starving or overloading any station.

This is where Packaging Line Automation Equipment comes together: feeding, weighing, bagging, inspection, transport, case packing and palletizing are treated as one system rather than separate machines. Multi-line distribution, reject handling after checkweighers and accumulation before robots are defined during project engineering, not after delivery.

Fabrication quality and compliance

Food-grade materials and washdown-capable construction are standard for most applications. Main structures use 304 stainless steel; contact surfaces are food-grade PU, PP/ABS or stainless steel. The fastback conveyor is IP54 rated, and other machines are sealed to the cleaning and exposure requirements of the product and plant.

Our core team has worked in automated packaging systems for nearly two decades. R&D, design and manufacturing are supervised by senior technical staff, and our technical file includes CE test report documentation and invention/utility model patents. Custom non-standard machines can be developed for unusual product sizes, line heights or plant constraints.

Information we use to configure your solution

We prepare every proposal from the working point of your line, not from a fixed product list. The following project data lets us select the correct conveyor type, elevator capacity, number of outlets, platform layout and robot configuration.

Project data How it shapes the equipment
Product type, bulk density, particle size and flowability Determines bucket volume, screw pitch, conveyor type and allowable transfer height.
Fragility, oil, coating or seasoning content Selects fastback, belt or screw handling and defines drop points.
Target throughput in kg/h, bags/min or cases/h Sets conveyor speed, number of outlets and robot cycle expectations.
Bag, case and pallet dimensions for each SKU Defines working width, changeover requirements and palletizing pattern.
Plant layout with floor plan and ceiling height Sets conveyor lengths, platform dimensions and discharge height.
Upstream and downstream machine interfaces Aligns belt speed, control signals, reject positions and accumulation length.
Washdown frequency, temperature and product exposure Confirms stainless grade, enclosure rating, sealing and contact materials.
Electrical supply and compressed air availability Defines motor rating, VFD settings, control cabinet and robot configuration.

Our scope can stop at a single conveyor or extend to integrated design and turnkey implementation of a full-plant automated packaging system. The standardized after-sales service system covers installation guidance, commissioning support, remote troubleshooting and spare parts.

Frequently asked questions

Can a fastback conveyor feed a multi-head weigher without breaking fragile product?

Yes. The horizontal motion advances product in a shallow tray without vibration or drops, which preserves fragile pieces and keeps seasoning or coating in place. The stainless steel tray is removable for cleaning between product runs.

Can one material distribution conveyor feed several packaging machines?

Yes. Speeds of 1-30 m/min and rotary blocking mechanisms allow the belt to divert product to different destinations, so a single supply source can feed multiple packaging machines or inspection devices in a flexible line layout.

What capacity range does a multi-outlet bucket elevator cover?

Bucket volume options of 1-6.5 L give production capacities of 2-12 m3/h depending on product density and lift height. The elevator is designed for granular materials and can interface directly with weighing machines or packaging machines.

Do you supply only conveyors or the full line from weigher to palletizer?

We supply both. System Equipment can be delivered as individual conveyor units or as part of a complete automatic packaging line, including packaging machines, weighing and dosing equipment, checking equipment and end-of-line robots.

What food-contact materials are used on the system equipment?

Main structures are 304 stainless steel, while contact parts use food-grade PU, PP/ABS or stainless steel depending on the product. This combination supports washdown cleaning and is suitable for food, frozen, agricultural and chemical applications.

Related Products and Categories

Our portfolio also includes Product for applications with different operating ranges, interfaces or integration requirements.